Start with measured commercial demand
Use the expected process throughput and a qualified commercial-product dose to estimate powder consumption per operating interval. Keep the units visible. If only a broad screening range is known, evaluate the corresponding demand range rather than presenting a single precise design figure.
Do not confuse dose to the process with stock concentration in a preparation tank. The dose-basis explanation separates commercial mass, documented active mass and prepared solution.
Calculate usable stock volume
For an explicitly mass-per-volume preparation, divide required commercial mass by the stated concentration. An illustrative 2 kg per hour demand at 2 g per litre needs 1,000 litres per hour of prepared stock. This is arithmetic only, not a recommended dose or make-down concentration.
If the preparation is defined by mass fraction, keep the calculation on that basis and obtain the information needed for any volume conversion. Do not silently assume a density or copy another grade’s concentration.
Check the complete preparation cycle
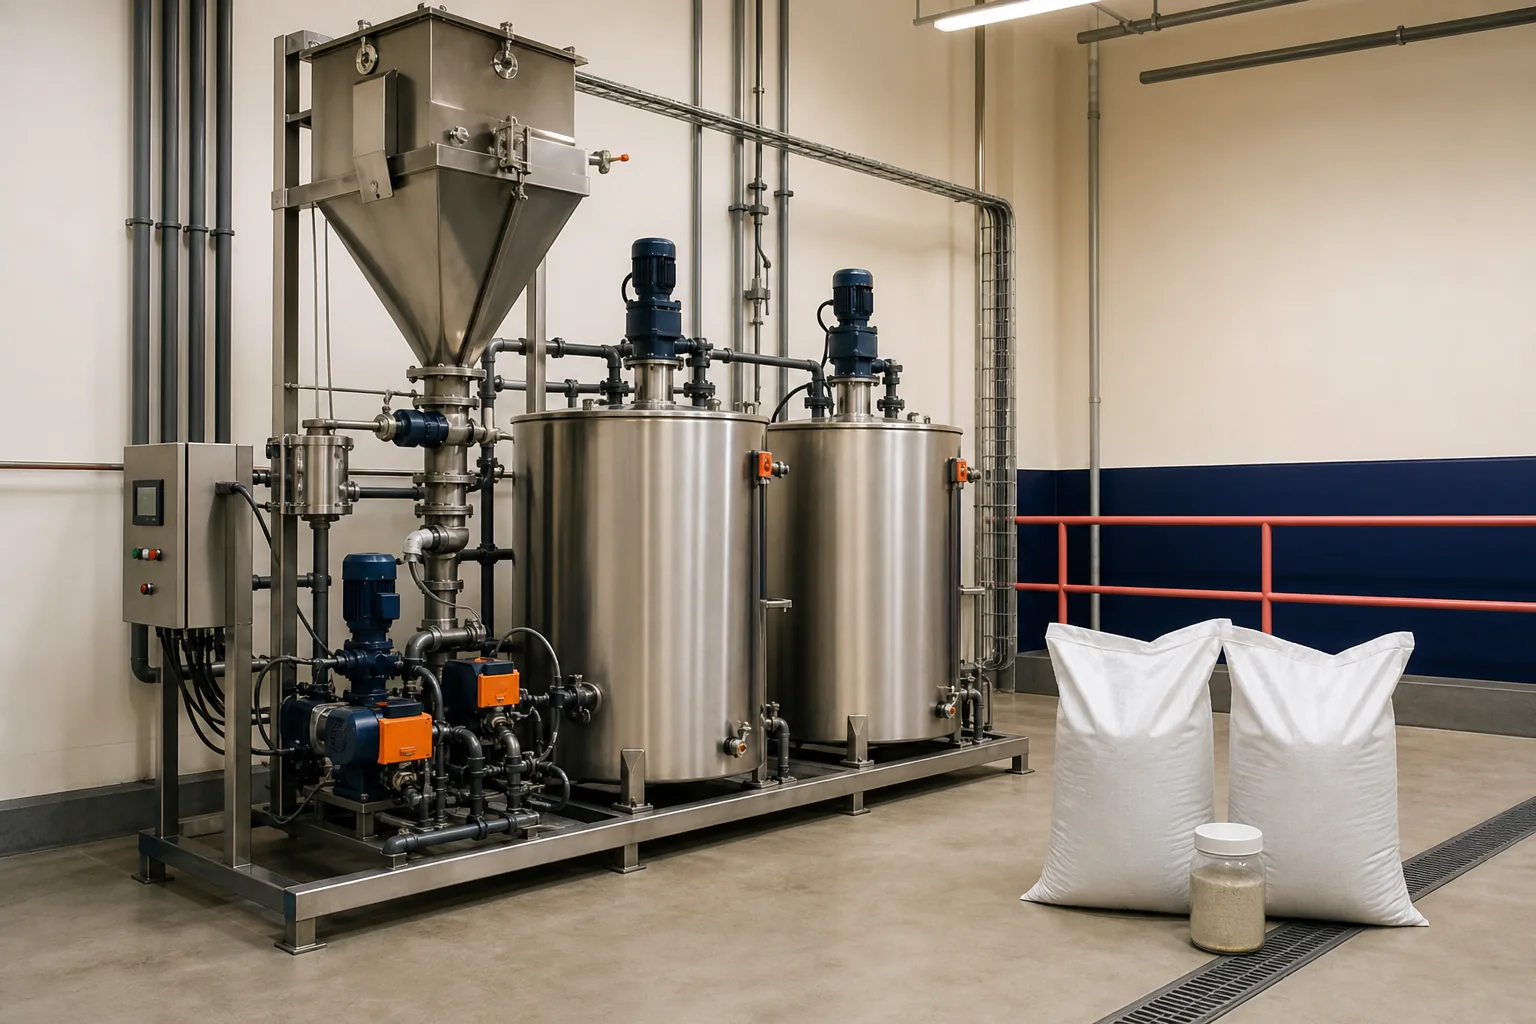
Account for working volume, powder dispersion, required hydration, transfer and the time before a batch is available. Check the ability to maintain supply during tank changeover or maintenance under plant procedures. A nominal tank size does not prove continuous usable output.
Verify water supply and actual pump delivery. Review the supplied-grade instructions and investigate inconsistent stock with powder-dispersion checks before interpreting a dose increase as an application requirement.
Match the purchase to the operating plan
Ask the supplier to review the intended preparation arrangement and proposed sample code. If a different concentration or form is needed, qualify that change before ordering the bulk quantity. Avoid promising throughput improvements from an unverified calculation.
Align packaging and replenishment with the confirmed demand and storage conditions. Include the preparation constraints in the quotation enquiry so a commercial offer does not assume equipment capability that the plant has not established.
Decision record for the quotation
| Decision | Evidence needed |
|---|---|
| Demand | Qualified commercial dose and process throughput define a transparent range. |
| Volume | Stock concentration and units support the calculation without hidden density assumptions. |
| Availability | Hydration, changeover, transfer and dosing are included in usable capacity. |